BOKNUTRA SINCE 2010
Our History: From Practical Manufacturing to Global Nutrition Partnerships
BOKNUTRA did not grow by trying to be everything at once. We grew by solving the next practical problem in front of our customers: making a formula workable, keeping a batch consistent, preparing the right documents, and building enough manufacturing depth to support the product after launch.
THE STARTING POINT
Good manufacturing starts before a production order.
When BOKNUTRA began in 2010, the nutrition business already had plenty of ingredient suppliers and factories. What many brand owners lacked was a manufacturing partner willing to stay involved between the idea and the finished product.
A promising concept can still fail for ordinary reasons. The active ingredient may not remain stable in the chosen format. A powder that looks fine on a laboratory bench may not flow evenly on a commercial line. A gummy may taste acceptable in the first sample but change during shelf-life testing. Packaging selected too early can add cost or delay registration. These are not glamorous problems, but they decide whether a product reaches the market on time.
That reality shaped how we built the company. Research, formulation, sourcing, quality, production, packaging and export support had to work as one connected process. Each stage needed a responsible team, clear records and a practical handover to the next stage.
OUR DEVELOPMENT
Seven milestones, one consistent direction
Every expansion answered a customer need we were already seeing in real projects.
Where the work began
BOKNUTRA was established to research, develop and manufacture nutritional health foods and special dietary foods. The early focus was straightforward: understand what the product needed to do, then build a production route that could deliver it reliably.
Formulation became a core capability
Customers needed more than a list of available ingredients. We expanded market insight, product development and formula-design support so projects could be evaluated for dosage, sensory performance, stability, cost and target-market requirements before scale-up.
Moving into automated multi-format production
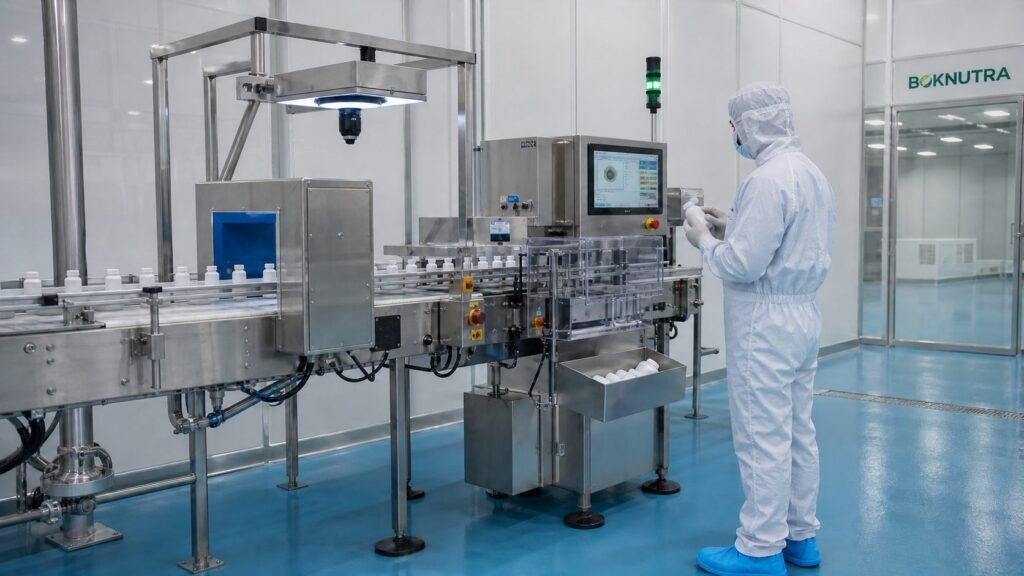
Demand was no longer limited to one delivery system. Automated capability expanded across soft capsules, hard capsules, tablets, powders, drops, bottled drinks, soft drinks, oral liquids and gummies. This allowed the format to follow the product strategy instead of forcing every idea into the same production line.
Quality control became a complete system
Testing was strengthened alongside a standardized control system covering R&D, procurement, production, inspection and sales. Raw-material approval, in-process checks, release testing and traceable records became connected parts of the same quality responsibility.
One coordinated OEM/ODM service
We brought market review, formulation, sampling, packaging development and commercial production into one project path. Customers gained a clearer owner for technical decisions and fewer handoffs between disconnected vendors.
A broader production and R&D network
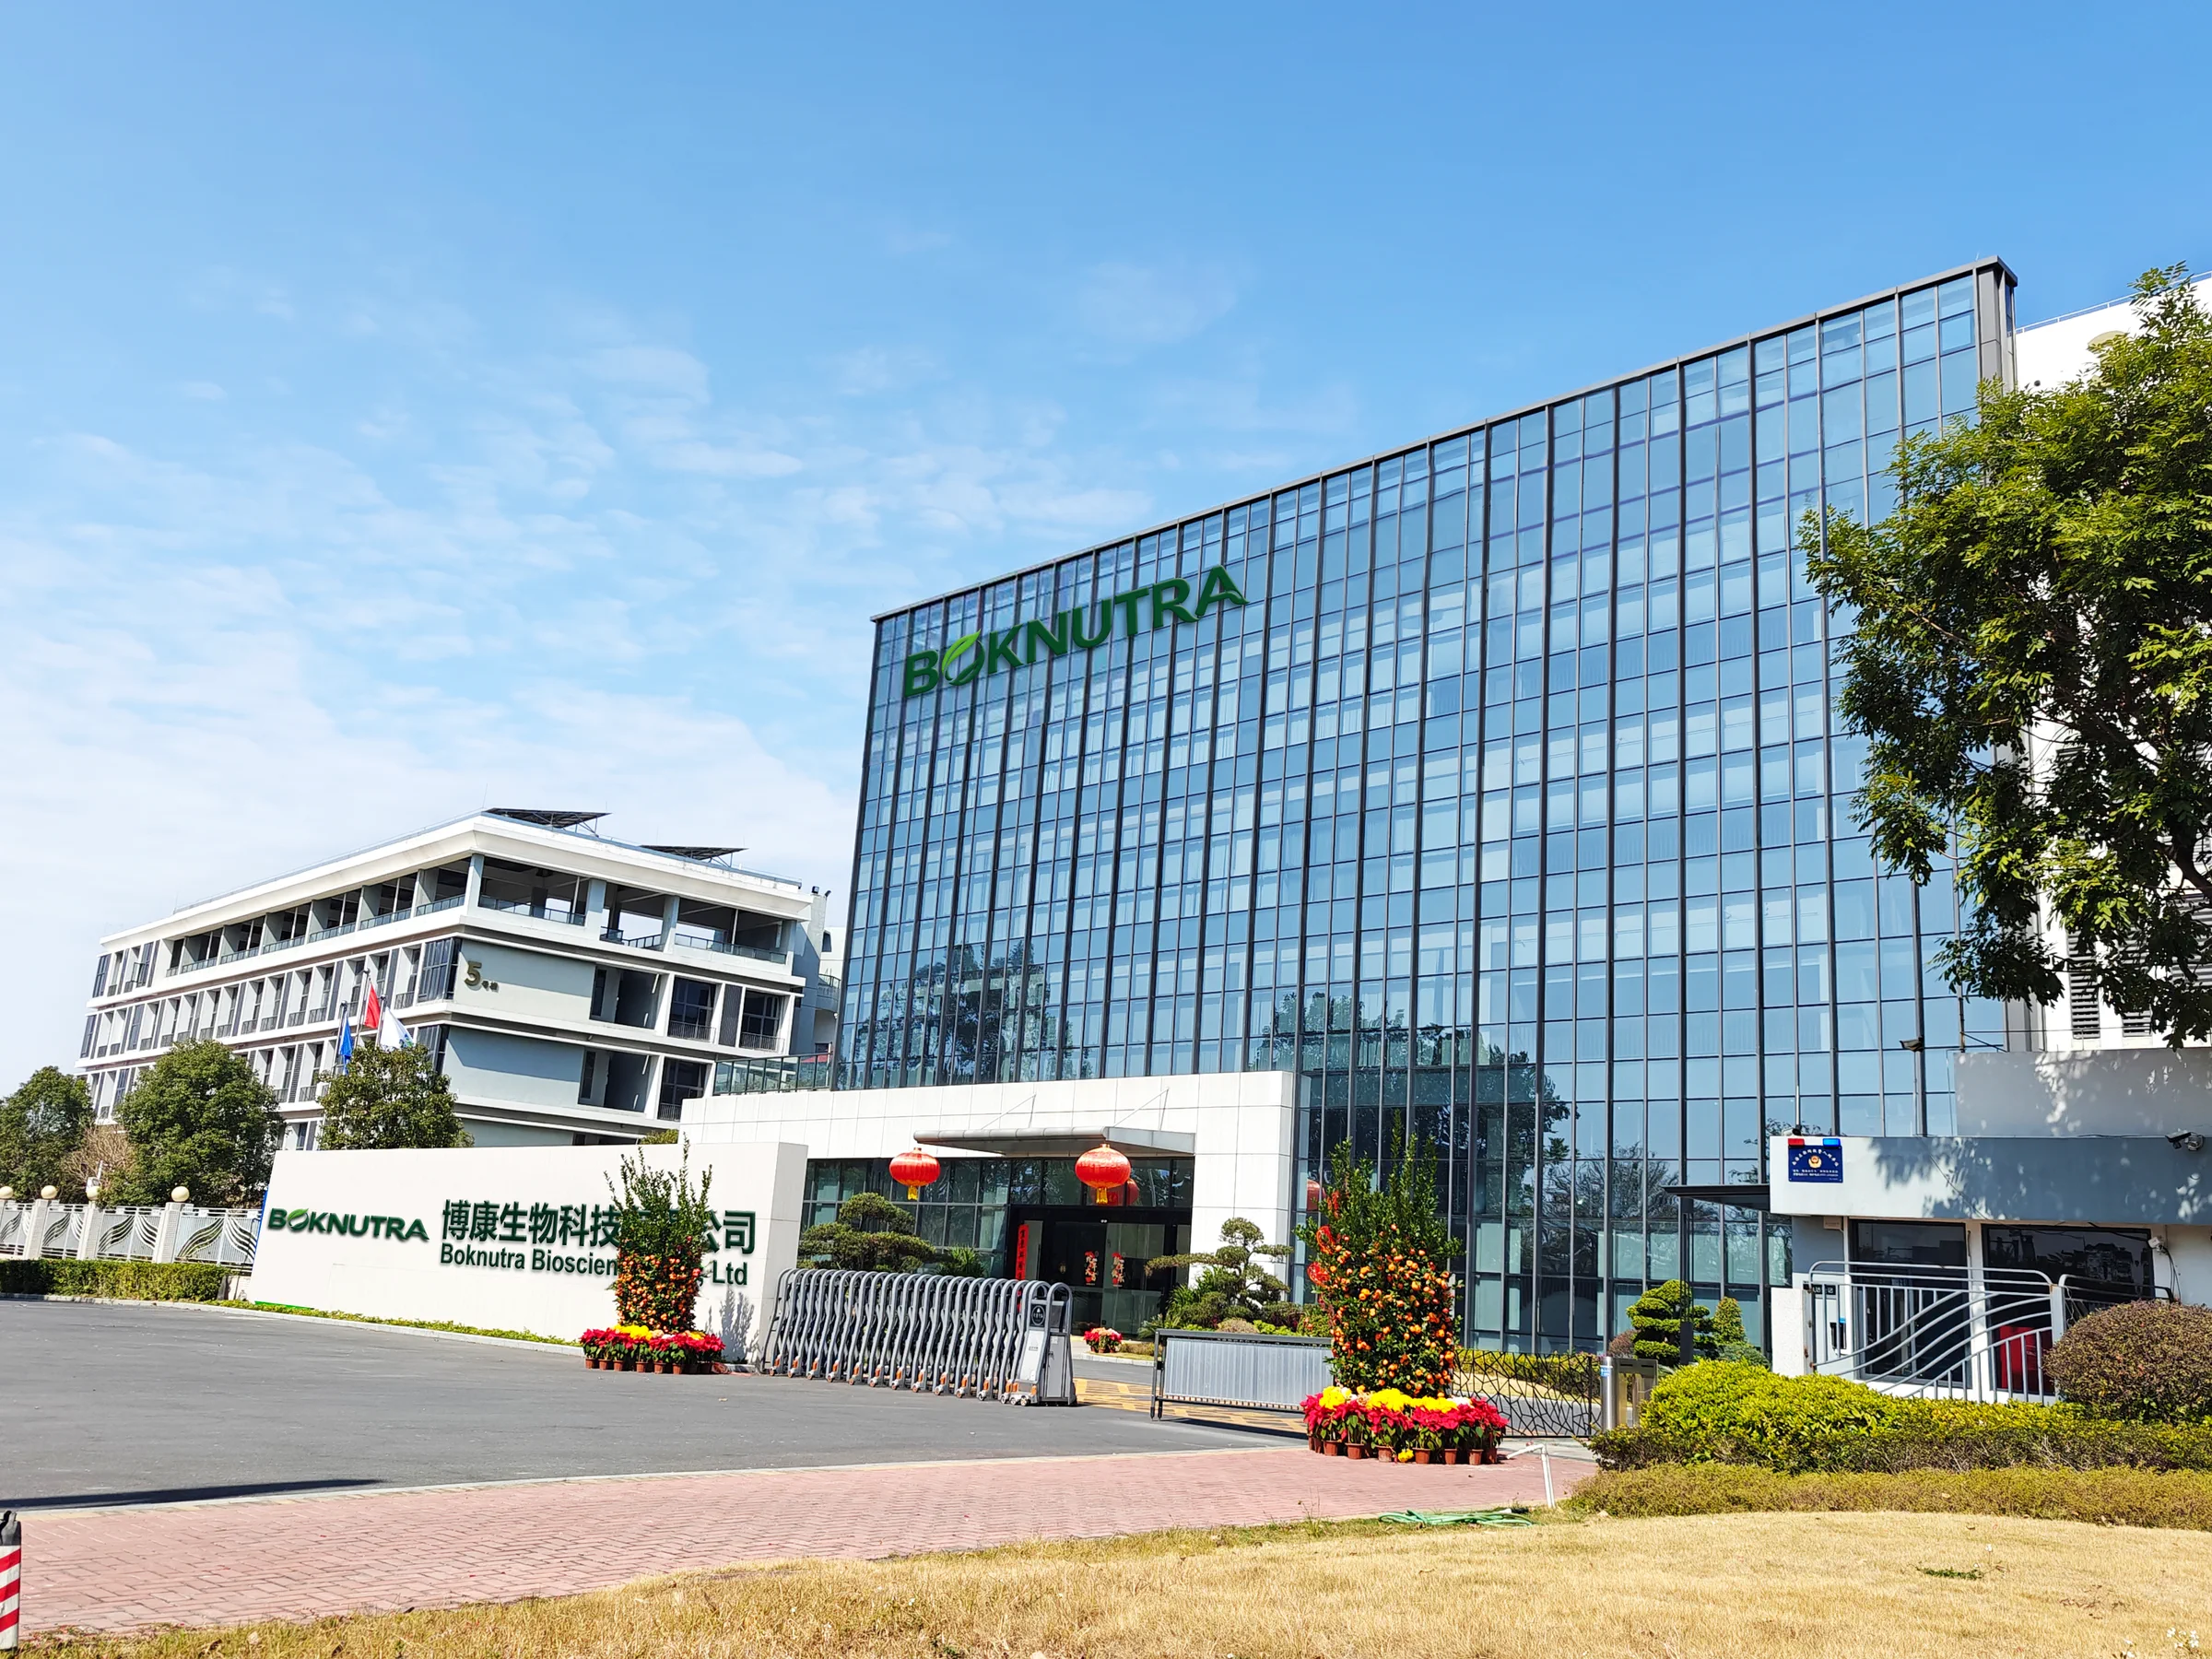
BOKNUTRA developed a network of five automated production bases and six R&D centers. The purpose was not scale for its own sake. It was to give projects access to the right technical team, production environment and capacity as requirements changed.
Supporting brands across global markets
Today, more than 10 intelligent production lines support over 10 dosage forms and a portfolio of more than 5,000 products. BOKNUTRA products are exported to over 100 countries across Europe, the Americas and other international markets.
BOKNUTRA TODAY
Scale that stays connected to the project
Capacity matters only when it can be translated into dependable batches, useful documentation and responsive decisions.
MANUFACTURING & R&D
More formats create better choices, not more confusion.
A brand may begin with a preferred format, but the best production decision depends on ingredient behavior, target dose, consumer use, shelf life, packaging and landed cost. Our R&D and manufacturing teams review those factors together.
That is why multi-format capability matters. Oils may need soft capsules or protected powder systems. High-dose ingredients may suit powders better than tablets. Drops and oral liquids can make dosing easier for specific users. Gummies and soft chews require careful work on flavor, texture, water activity and stability.
Before commercial production, the team aligns the formula, process parameters, specifications, test methods and packaging requirements. The goal is simple: the product approved in development should be the product the customer can continue ordering.
QUALITY IN PRACTICE
Quality is not a final inspection department.
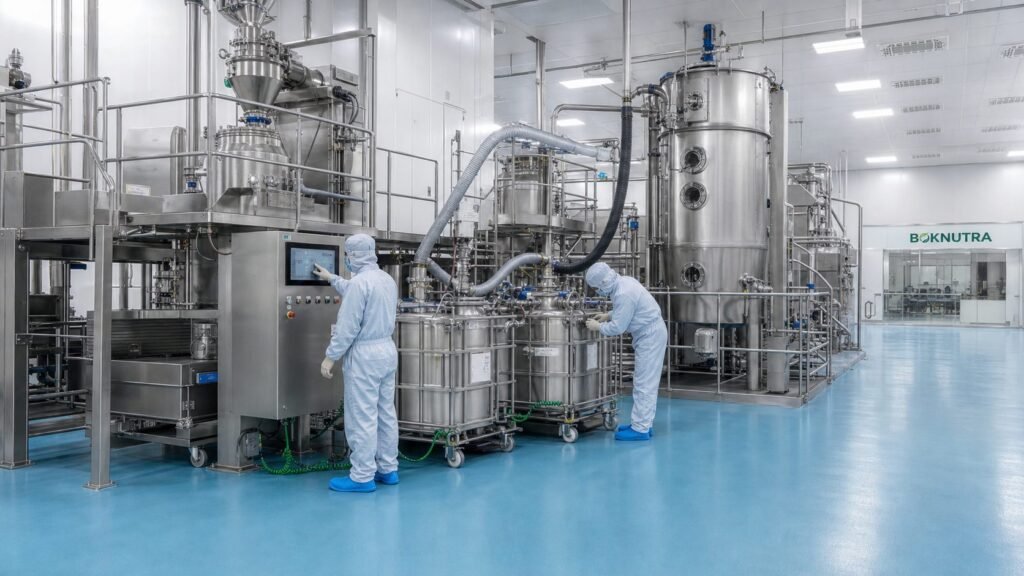
It begins with supplier qualification and raw-material identity. It continues through weighing, mixing, filling, tableting, encapsulation, packaging and batch release. When a result falls outside an approved limit, the question is not only whether the batch passes. The team must understand why the result changed and prevent the same issue from moving forward.
Our testing center is built to CNAS laboratory accreditation standards and is equipped for gas chromatography, liquid chromatography, heavy-metal analysis and other professional testing. The laboratory performs physicochemical analysis, microbiological examination and active-component determination so raw materials and finished products can be assessed quickly and accurately.
For B2B customers, this system supports something very practical: repeatability. A successful first batch is useful. A controlled process that can reproduce it across future orders is what protects a brand.
QUALIFICATIONS & MARKET ACCESS
Systems customers can examine, not promises they have to take on trust
BOKNUTRA has obtained more than 20 domestic and international qualifications. They support quality management, food safety, responsible operations and access to different markets.
Quality & food safety
- ISO 9001
- ISO 22000
- FSSC 22000
- HACCP
- cGMP
- BRCGS
Responsible operations
- ISO 14001
- ISO 45001
- SEDEX
- Energy Management System
- Intellectual Property Management System
International market access
- FDA Registration
- Non-GMO
- EU Organic
- USDA Organic
- JAS Organic
- Kosher
- Halal
- EU Aquatic Product Registration
- Canadian FSRN Registration
Certification and registration scope may vary by legal entity, facility, production line, product category and destination market. Current certificates and applicable scope are confirmed during project qualification.
WHAT THIS HISTORY MEANS FOR CUSTOMERS
A more experienced partner should make the work clearer.
Most customers do not need another factory presentation. They need clear answers. Can the target dose be produced in the preferred format? Will the texture, flavor and appearance remain stable? Can future batches follow the approved specification? Which documents are available for the destination market? Who owns the next action when a technical issue appears?
That is the thread running through BOKNUTRA’s history. We have added facilities, formats, laboratories and qualifications, but the reason for adding them has stayed the same: help customers move from a product idea to a reliable commercial supply with fewer gaps in between.